Featured Industrial Pallet Racking Systems
Precision-engineered structural steel warehouse systems calculated to EN 15512, FEM 10.2.02, and ANSI MH16.1 standards. Designed for high volume, heavy loads, and maximized vertical footprint.
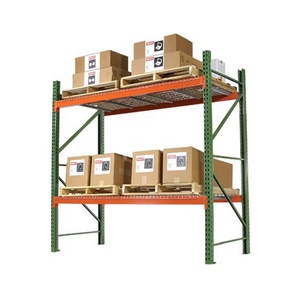
Steel Selective Pallet Rack Adjustable Heavy Duty Storage Shelving System
Direct access to every pallet position. Cold-rolled Q235B/Q355B steel frame featuring adjustable beam pitch at 50mm/75mm intervals.
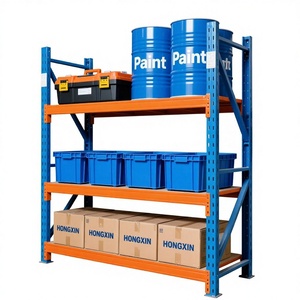
Low Price 4 Layer Steel Storage Rack Adjustable Boltless Warehouse Shelving
Corrosion-resistant powder-coated boltless modular framework. Optimized for rapid assembly, medium-duty hand picking, and archival storage.
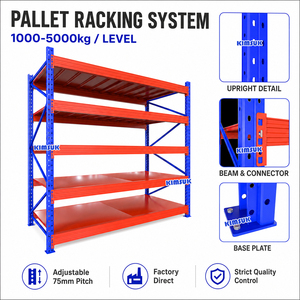
Heavy Duty Rack Laminated Aluminum & Steel Warehouse Shelving Units
High-strength laminated decking options designed for extreme structural loads. Resistant to impact, thermal fluctuation, and moisture.
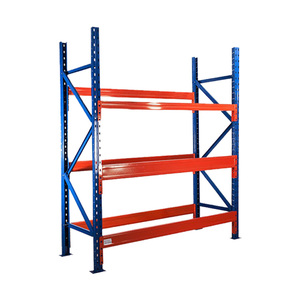
Metal Racks System Warehouse Shelving with Free Storage Solution Design
Tailor-made industrial racking configuration backed by complete structural CAD & 3D BIM engineering. Ideal for manufacturing & fulfillment centers.
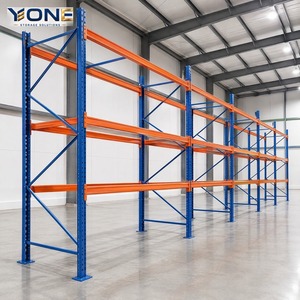
Steel Storage Rack Warehouse Selective Pallet System for Industrial Organizers
Standard industrial structural rack configuration engineered to support standard Euro, GMA, and Australian perimeter-base pallets up to 2500kg/level.
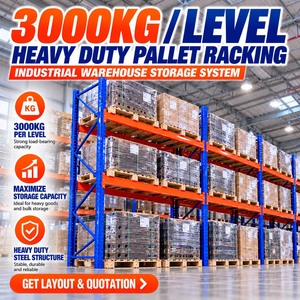
3000kg Per Level Heavy Duty Warehouse Pallet Racking System
Ultra-heavy-duty reinforced box-beam architecture constructed for heavy machinery parts, metal stamping dies, and dense raw materials.
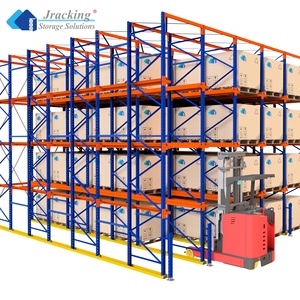
Heavy Duty Industrial Steel EU Blue & Orange Selective Pallet Racking CE Certified
CE and ISO certified rack structure featuring safety locking pins, high visibility powder coating, and heavy-duty floor anchor footplates.
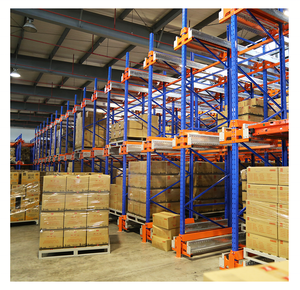
Automated Warehouse Storage System Steel Radio Shuttle Pallet Rack
Semi-automated deep lane storage solution utilizing wireless radio shuttles. Maximizes storage density while drastically reducing forklift operational cycles.
Engineering Leadership & Manufacturing Capabilities in China
As a tier-one China pallet rack system manufacturer and global wholesaler, our production infrastructure bridges state-of-the-art metallurgical processing with rigorous structural engineering. Modern supply chain logistics require storage infrastructures that do not simply hold static inventory, but actively optimize floor cube utilization, structural resilience, and operational safety. Our manufacturing facilities are equipped with continuous cold roll-forming lines, automated robotic welding cells, and electrostatic powder coating complexes certified under ISO 9001:2015 and ISO 14001 quality management systems.
Certified High-Tensile Steel
We source prime structural steel exclusively from top-tier state mills (BaoSteel, Shougang Group). Utilizing high-yield strength Q235B and Q355B grade steel ensures optimal load-to-weight ratios, minimal beam deflection under full capacity, and superior fatigue resistance during dynamic forklift operations.
Automated Robotic Welding
Every beam connector claw and baseplate joint is executed via automated robotic MIG welding systems operating under ISO 3834-2 welding quality requirements. This eliminates human margin of error, ensuring 100% full-penetration weld integrity across high-stress connection points.
Surface Protection Tech
Our 9-stage pre-treatment wash includes automatic iron-phosphate conversion coating followed by thermosetting epoxy-polyester powder coating (60–90 microns). Tested under ASTM B117 salt spray standards for over 500 hours without corrosion creep.
Technical Comparison of Industrial Warehouse Racking Systems
Selecting the correct warehouse pallet rack configuration requires balancing SKU velocity, storage density, building ceiling clear height, and total equipment investment. The technical matrix below provides an objective engineering comparison between standard structural pallet storage architectures.
| Storage System Type | Storage Density | SKU Selectivity | Typical Load Capacity | Forklift Clearance Requirement | Optimal Application Scenario |
|---|---|---|---|---|---|
| Selective Pallet Rack | Standard (40-50%) | 100% Direct Access | 1,000kg – 4,500kg / Level | 3.0m – 3.5m (Standard Counterbalance) | High-SKU 3PL, FMCG distribution, retail logistics. |
| Radio Shuttle Rack | Ultra-High (75-85%) | Low (Batch Selective) | 1,500kg / Pallet Position | Main Aisle Only (Minimal travel inside lanes) | Cold storage (-25°C), high-volume homogeneous goods. |
| Drive-In / Drive-Thru | High (65-75%) | Low (LIFO / FIFO) | 1,000kg – 1,500kg / Position | Truck enters racking structure directly | Bulk seasonal inventory, low SKU turn items. |
| Push-Back Racking | Medium-High (60-70%) | Moderate (2-6 Deep) | 1,000kg – 1,500kg / Cart | Standard Aisle (Telescopic cart system) | Medium SKU count with high pallet counts per SKU. |
| Automated ASRS System | Maximum (85-95%) | 100% Automated | 500kg – 3,000kg / Position | Zero Forklift Aisles (Crane / RGV Operated) | High-bay automated distribution, 24/7 dark operations. |
Future Procurement Trends in Pallet Racking & Logistics
The industrial storage sector is undergoing a rapid paradigm shift driven by land cost appreciation, labor availability challenges, and stringent ESG compliance mandates. When procuring pallet rack systems from China manufacturers, global supply chain executives must account for three structural trends shaping the 2025–2030 warehousing landscape:
1. Hybrid Shuttle & ASRS Integration
Traditional static racking is increasingly giving way to hybrid semi-automated storage. Warehouses are retrofitting heavy-duty pallet rack frames with self-charging 4-way radio shuttles and automated guided vehicles (AGVs). This transition yields up to 40% reduction in warehouse operational energy consumption while elevating vertical storage heights up to 40 meters.
2. Sustainable & Green Steel Compliance
Scope 3 emissions accounting has reached industrial supply chains. Top Chinese manufacturers are pioneering the use of low-carbon recycled steel billets processed via Electric Arc Furnaces (EAF). Furthermore, zero-VOC solvent-free powder coatings are becoming mandatory standard practice for international enterprise RFQs.
3. Dynamic Seismic Resilience & IoT Health Monitoring
Modern rack installations in earthquake-prone regions (seismic zones Z1 through Z4) now demand higher ductility factors under EN 1998 and SIA 261 standards. Leading rack systems now incorporate real-time strain gauge sensors and displacement monitoring to instantly detect forklift impact damage or structural overload conditions.
Frequently Asked Questions for Global Procurement
Key structural, logistics, and compliance considerations when sourcing heavy-duty pallet racking systems directly from China manufacturers.
What structural standards do your pallet rack systems comply with?
Our storage racks are structural-engineered in strict accordance with the European EN 15512 standard (Steel static storage systems - Adjustable pallet racking systems - Principles for structural design), FEM 10.2.02 codes, RMI (Rack Manufacturers Institute ANSI MH16.1), and ISO 9001 guidelines. Complete static structural load calculations and material mill test certificates (MTC) are provided with every order.
How do you calculate maximum frame load capacities for custom layouts?
Frame load capacity depends on several structural variables: clear beam elevation height, maximum unit load weight per pallet, distance between beam levels, seismic acceleration coefficients of your geographical zone, and floor slab thickness. Our engineering team utilizes finite element analysis (FEA) software to calculate exact column cross-sections (e.g., 80x60, 90x70, 100x70, 120x95 profile dimensions) and wall thicknesses (1.5mm to 3.0mm) needed to ensure a safety factor of 1.5 to 2.0.
Can racking structures be customized for cold storage (-25°C to -30°C) environments?
Yes. Sub-zero environments cause standard carbon steel to undergo ductile-to-brittle transition. For cold storage and blast freezer applications, we specify low-temperature impact-tested steel grades (such as Q355D or Q355E) combined with specialized low-temperature powder coatings and hot-dip galvanizing options to prevent embrittlement, thermal stress cracking, and micro-rusting.
What is the typical production lead time and shipping packaging for wholesale orders?
Standard manufacturing lead times range from 14 to 25 calendar days depending on project volume (typically 2 to 10 40ft High Cube containers). All racking components are bundled using plastic steel banding, heavy-duty cardboard edge protectors, and stretch-wrap film. Beams and uprights are loaded onto custom timber/steel runners to facilitate safe forklift unloading at the destination port or jobsite.
Do you provide installation support, foundation design, and site maintenance guidelines?
We supply fully detailed installation blueprints, 3D step-by-step assembly guides, torque specifications for anchor bolts, and video documentation. For major warehouse developments, we offer on-site installation supervision by senior structural technicians. We also provide complete annual inspection protocols compliant with EN 15635 for ongoing operational safety management.
Optimize Your Warehouse Floor Space Today
Contact our engineering team for free technical consultations, customized warehouse layout CAD drawings, and factory-direct wholesale pricing within 24 hours.
Get a Quote